Blind fasteners explained for one-sided metal assembly
a[data-rs-seo-link]{text-decoration:underline!important;color:#1a56db!important;cursor:pointer!important;}a[data-rs-seo-link]{text-decoration:underline!important;color:#1a56db!important;cursor:pointer!important;}
What blind fasteners are and when they solve a real assembly problem
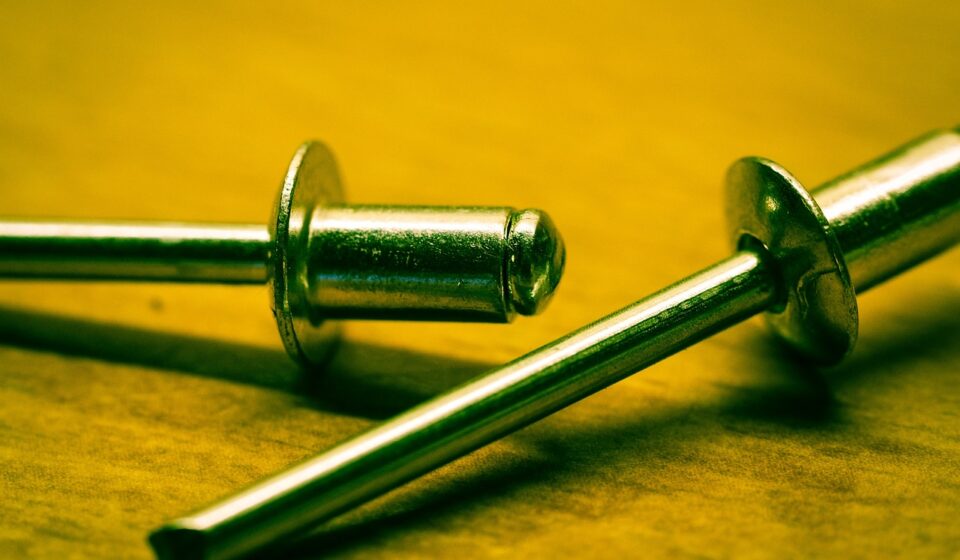
Blind fasteners are mechanical fasteners installed from one accessible side of a workpiece. That one-sided installation is their main value. Instead of needing a wrench, bucking bar or installer behind the joint, the fastener expands, pulls, collapses or locks on the blind side during setting. In sheet metal, hollow sections, closed enclosures, panels, ducts, vehicle bodies and field repairs, this can simplify assembly and, in some cases, make the joint possible at all.
The design question is not simply whether blind fasteners are convenient. The selected fastener still has to match the joint’s load, material, thickness, environment and inspection requirements.
In purchasing and design language, the term covers several related product families. Break-mandrel blind rivets are the most familiar. Structural blind rivets and blind bolts are used where higher load transfer or retained mandrel features are required. Rivet nuts add a reusable internal thread to thin material. Each family solves a different problem, so treating all blind products as interchangeable can lead to weak joints, loose panels or premature corrosion.
For more general fastening context, see the Fasteners section.
How blind fasteners work
Most blind fasteners start with a prepared hole. The installer inserts the fastener from the accessible side, applies a setting tool, and the blind-side portion changes shape or locks into position. In a break-mandrel blind rivet, the tool pulls the mandrel through the rivet body. The body expands against the blind side, clamps the sheets, and the mandrel breaks at a designed point. In many rivet nuts, the tool pulls on the internal thread so the sleeve collapses and grips the sheet. In blind bolts and lockbolt-style designs, a pin, sleeve or collar system forms a more structural connection.
The visible process is simple, but the finished joint depends on several variables. Hole diameter, grip range, sheet hardness, coating thickness, tool stroke and blind-side condition all affect the result. A rivet that looks seated can still be under-set, over-set or outside its intended grip range. For that reason, manufacturers publish application data for each part number, and blind fastening should be treated as a joining process rather than a commodity purchase.
Main types of blind fasteners
The most useful way to compare blind fasteners is by function, not only by shape. The table below summarizes common options used in industrial and sheet metal work.
| Type | Typical use | Key advantage | Main caution |
|---|---|---|---|
| Open-end blind rivet | General sheet metal, light covers, brackets and housings | Fast installation and broad availability | Usually not sealed; strength depends heavily on correct grip and hole size |
| Closed-end blind rivet | Assemblies needing better splash, dust or mandrel retention control | Blind end is closed after setting | Not automatically suitable for pressure sealing unless specified and tested |
| Multi-grip blind rivet | Assemblies with variable stack thickness | Can cover a wider grip range than many standard rivets | Still must be matched to the approved grip range |
| Structural blind rivet | Higher-load panels, transport equipment and fabricated structures | Often offers improved shear, tensile or mandrel retention performance | Requires closer attention to tool, hole and inspection requirements |
| Blind bolt or blind lockbolt | Applications needing bolt-like load transfer with one-sided access | Can support heavier-duty joints than ordinary blind rivets | Larger holes, higher installation force and higher cost may apply |
| Rivet nut | Thin sheet requiring a reusable thread | Adds a female thread where tapping is not practical | Can spin or pull out if torque, hole condition or sheet thickness is wrong |
This table is only a starting point. Two rivets with the same nominal diameter can have different shear strength, mandrel retention, head style, corrosion resistance and recommended hole size. In regulated or safety-related applications, selection should follow the controlling drawing, specification or approved part list.
Selection criteria that matter in real joints
Access and joint geometry
Blind fastening is useful when the back side is closed, obstructed or unsafe to reach. The blind side still needs enough room for the formed head, bulb or sleeve. A fastener that works in a flat lap joint may not work in a narrow tube, folded channel or cavity with internal wiring. Designers should check blind-side clearance before finalizing the hole pattern.
Grip range and stack thickness
Grip range is the total material thickness the fastener is designed to clamp. If the stack is too thin, the fastener may not form correctly or may loosen. If the stack is too thick, the blind-side head may be incomplete and clamp load may be inadequate. Coatings, adhesive layers, gaskets and paint should be included when estimating stack thickness, especially in assemblies with variable material lots.
Shear, tensile and peel loads
Blind rivets often perform well in shear when the joint design keeps the load across the shank. Tensile pull-out, peel and prying loads are more demanding because they try to open the joint. A higher published shear value does not automatically mean the joint will survive peel or fatigue. Where the joint sees vibration, cyclic loading or structural load transfer, testing the actual joint stack is safer than relying only on catalogue ratings.
Material and corrosion compatibility
Common blind fastener materials include aluminum, carbon steel and stainless steel, often with different mandrel materials. Mixed metals can create galvanic corrosion when an electrolyte is present. This matters in outdoor equipment, marine-adjacent environments, HVAC units, transport bodies and assemblies exposed to road salts or washdown. Coatings can help, but they should be evaluated together with the base material, joint design and service environment.
Installation tool control
A blind fastener is only as reliable as the installation process. Manual tools may be adequate for maintenance or low-volume work, while pneumatic, hydraulic or battery tools are common in production. Tool nosepiece condition, pulling force, stroke, alignment and operator technique can all change the final joint. On production lines, periodic tool checks and sample inspections reduce the risk of under-set fasteners moving downstream.
Standards and test references to know
Standards do not choose a fastener for a design, but they provide shared language and test methods. ISO 14588:2000 covers terminology and definitions for blind rivets; the ISO catalogue lists it as reviewed and confirmed in 2026, so it remains a current reference at the time of writing. ISO 14589:2000 addresses mechanical testing of blind rivets. ISO 13469:2014 covers testing procedures for form-fit blind rivet joints and lock bolt joints, including metallic and non-metallic materials.
These references are useful because blind fastening is not only a single-part performance question. ISO 13469, for example, frames testing around the joint and the performance requirements of the component or assembly. That approach is important in real applications: a rivet may meet its own product specification and still be unsuitable if the sheet material, hole preparation, edge distance or service load is wrong.
In North American practice, Industrial Fasteners Institute, SAE, aerospace and defense-related standards may also appear on drawings or purchasing documents. The relevant standard depends on industry, geography and application. Commercial sheet metal work, aerospace repair, transportation bodies and consumer products may use different specifications even when the fastener looks similar. See also: Buying Guides.
Where blind fasteners are commonly used
Blind fasteners are widely used where one-sided access, speed and clean assembly are more important than disassembly. Typical applications include cabinets, appliance panels, vehicle bodywork, trailers, HVAC ducting, electronic enclosures, signage, access panels, lightweight frames and repair patches. Rivet nuts are common where thin sheet needs a serviceable screw connection for covers, brackets or components that may be removed later.
They also support design-for-assembly goals. A manufacturer can reduce the need for workers to reach behind panels, eliminate loose nuts in closed cavities and automate or semi-automate repetitive fastening points. In field maintenance, a technician can often install a blind rivet from the accessible side without dismantling a larger assembly.
Convenience, however, should not be confused with universal suitability. If a joint requires high clamp load, frequent removal, precise preload, full visual inspection of both sides or predictable high-cycle fatigue performance, a conventional bolt, welded joint, clinch fastener or engineered insert may be more appropriate. The correct choice depends on the joint’s job, not only on installation speed.
Common failure modes and how to reduce them
Many blind fastener failures start before installation. Oversized, misaligned or burred holes reduce bearing area and can prevent the fastener from expanding correctly. Poor edge distance can lead to sheet tear-out. Installing outside the grip range can leave the joint loose even if the visible head appears flush. Soft or brittle materials may crush, crack or creep under the formed blind head.
- Loose joints: Check grip range, tool setting, hole size and whether the stack includes compressible layers.
- Mandrel issues: Use the specified tool and nosepiece; verify whether the application requires retained mandrels or a closed-end design.
- Corrosion staining: Review base material, fastener material, coating and exposure to moisture or salts.
- Rivet nut spin-out: Confirm hole shape, sheet thickness, installation stroke and service torque limits.
- Panel distortion: Consider head diameter, clamp load, washer use, material thickness and installation sequence.
For critical assemblies, sample testing provides the clearest information. A basic test program can compare candidate fasteners in the actual materials, thicknesses, coatings and hole preparation used in production. Pull-out, shear, torque-to-turn, leak checks, vibration exposure or salt-spray evaluation may be relevant depending on the product. Testing should be documented before the design is frozen, not after field complaints appear.
A practical specification checklist
When specifying blind fasteners, a clear callout reduces purchasing mistakes and production variation. At minimum, identify the fastener family, nominal diameter, grip range, body material, mandrel or pin material, head style, finish, standard or manufacturer part number, hole size and installation tool requirements. If the joint has sealing, electrical grounding, cosmetic or corrosion requirements, include those requirements directly rather than assuming they are implied.
A useful engineering review asks six questions. What load path will the fastener carry? Can the blind side form freely? Is the joint stack thickness stable or variable? Are the metals compatible in the service environment? Can production verify the set condition? What happens if the fastener must be removed or repaired? If the answers are unclear, the safest next step is not to choose a larger rivet by instinct, but to confirm the joint design and test method.
Frequently asked questions
Are blind fasteners the same as blind rivets?
Not exactly. Blind rivets are one major type of blind fastener, but the broader category also includes rivet nuts, blind bolts and some lockbolt-style products. The shared feature is one-sided installation; the joint behavior can be very different.
Can blind fasteners replace bolts?
Sometimes, but not automatically. Blind bolts may be suitable for some bolt-like applications, while ordinary blind rivets are usually permanent joining fasteners rather than preload-controlled threaded fasteners. Load, inspection, removability and service conditions should guide the choice.
Are blind rivets waterproof?
Some closed-end or sealed designs can improve resistance to moisture paths, but a blind rivet should not be assumed waterproof without manufacturer data and joint testing. Hole quality, surface finish, gasket use and installation consistency all affect sealing performance.
What is the most common mistake when selecting blind fasteners?
The most common mistake is choosing by diameter and material alone. Grip range, hole size, joint stack, load direction, installation tool and environmental exposure are just as important to the final joint.
Can blind fasteners be removed?
Many blind rivets can be drilled out, and rivet nuts can sometimes be removed with more involved repair work, but removal may enlarge holes or damage the base material. If routine disassembly is expected, a threaded solution should be designed into the assembly from the beginning.
Bottom line
Blind fasteners are valuable because they make one-sided assembly practical, fast and repeatable. Their strongest applications are joints where the back side is inaccessible and the fastener has been matched to the load, material, grip range and environment. The safest selection process compares product families first, then verifies the chosen part with standards, manufacturer data and, where necessary, joint-level testing. Used that way, blind fastening is not just a workaround for limited access; it is a deliberate design choice for efficient metal assembly.